


boiler water treatment chemicals
Boiler Water Treatment Chemicals Essential for Efficient Operations
Boilers are critical components in various industrial processes, generating steam for heating, power generation, and manufacturing. However, the efficiency and longevity of a boiler largely depend on the quality of water used and the application of appropriate treatment chemicals. Boiler water treatment chemicals play a vital role in maintaining optimal performance, preventing scale formation, corrosion, and other detrimental issues associated with boiler operation.
The primary concern in boiler water treatment is the presence of dissolved solids, including minerals such as calcium, magnesium, and iron. When water is heated, these minerals can precipitate and form scales on the boiler tubes, restricting heat transfer and reducing efficiency. This scaling can lead to serious operational issues, including overheating and potential boiler failure. To combat this, various treatment chemicals are employed.
One of the most common classes of boiler water treatment chemicals is scale inhibitors. These compounds work by interfering with the crystallization of minerals, essentially preventing them from forming solid scales. Phosphonates and polyacrylic acids are widely used as scale inhibitors, as they can effectively keep dissolved minerals in a state that does not precipitate onto boiler surfaces. Another effective strategy is the use of dispersants, which help to keep particles suspended in the water, preventing them from adhering to surfaces.
Corrosion is another significant concern in boiler systems. Water can be corrosive due to dissolved gases such as oxygen and carbon dioxide. Oxygen, for instance, can cause pitting corrosion, leading to failures in boiler materials over time. To address this, oxygen scavengers, such as sodium sulfite or hydrazine, are often introduced into the boiler water. These chemicals react with oxygen, effectively removing it from the system and reducing the risk of corrosion.
boiler water treatment chemicals

Furthermore, the pH level of the boiler water is crucial for maintaining a balanced environment. Monitoring and adjusting the pH can prevent both scaling and corrosion. Alkalinity boosters, such as caustic soda or sodium bicarbonate, are used to raise the pH and maintain proper caustic levels. A stable pH not only enhances the effectiveness of other treatment chemicals but also protects the integrity of the boiler system.
The choice of boiler water treatment chemicals also depends on the specific type of boiler and its operational conditions. High-pressure boilers, for example, may require more sophisticated treatments compared to low-pressure systems. Similarly, the source of the feedwater—whether it is from a river, well, or municipal supply—will influence the treatment program. Therefore, it is essential for operators to conduct thorough water analysis before selecting appropriate chemicals.
The effectiveness of boiler water treatment also relies on proper monitoring and maintenance procedures. Regular analysis of water chemistry is necessary to ensure that the treatment program is achieving its desired outcomes. Using online monitoring systems can provide real-time data, enabling rapid adjustments to the chemical dosing as needed. This proactive approach not only enhances boiler performance but also extends the life of the equipment, resulting in significant cost savings.
In conclusion, boiler water treatment chemicals are indispensable for industries reliant on boiler systems. By preventing scaling, controlling corrosion, and optimizing water chemistry, these chemicals ensure efficient boiler operation and minimize maintenance costs. A well-implemented water treatment program, tailored to the specific needs of the boiler and its operational environment, will contribute significantly to the overall productivity and reliability of industrial processes. Investing in the right chemicals and monitoring systems is essential for any organization looking to enhance its boiler performance and safeguard its operations.
-
How to Choose Dimethyl Disulfide DMDS for Industrial UseNewsNov.09,2026
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
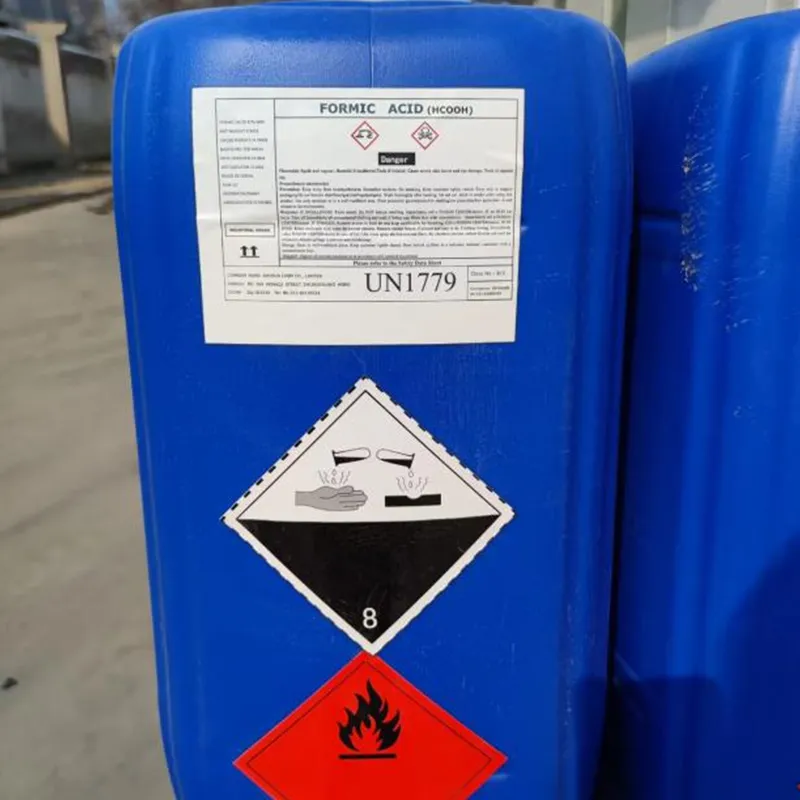
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.