


Understanding the Role and Applications of Chemical Solvents in Various Industries
Chemical Solvents An In-Depth Exploration
Chemical solvents play a critical role in various industrial processes and laboratory applications. They are substances that dissolve a solute, resulting in a solution. Solvents can be classified into various categories based on their chemical properties, including polar, non-polar, protic, and aprotic solvents. Their versatility and utility make them indispensable in several fields, including pharmaceuticals, petrochemicals, coatings, and cleaning products.
Types of Chemical Solvents
1. Polar Solvents Polar solvents, such as water, methanol, and ethanol, have molecules with a significant difference in electronegativity, leading to a positive and negative end. Their ability to dissolve ionic compounds and polar substances makes them essential in biochemical reactions and analytical chemistry. In pharmaceutical industries, polar solvents are often used in the synthesis of drugs, enabling the formation of complex molecular structures.
2. Non-Polar Solvents Contrary to polar solvents, non-polar solvents such as hexane, benzene, and toluene, have no significant charge separation within their molecules. This characteristic allows them to effectively dissolve non-polar compounds, making them widely used in organic chemistry and the formulation of paints, inks, and adhesives. Non-polar solvents are integral in the extraction processes where plant oils need to be separated from non-polar triglycerides.
3. Protic and Aprotic Solvents Protic solvents contain hydrogen atoms bonded to electronegative atoms like oxygen or nitrogen, enabling them to participate in hydrogen bonding. Water and alcohols are prime examples of protic solvents. Aprotic solvents, on the other hand, lack these acidic hydrogen atoms and include solvents like acetone and dimethyl sulfoxide (DMSO). The choice between protic and aprotic solvents can significantly affect the kinetics and mechanisms of chemical reactions.
Applications of Chemical Solvents
Chemical solvents find applications in numerous industries.
chemical solvents
- Pharmaceuticals In drug formulation and synthesis processes, solvents help in dissolving raw materials, participating in chemical reactions, and ensuring proper mechanical properties of the final products. For instance, solvents like ethanol are often used in extracting active ingredients from plant materials for herbal medicine preparations.
- Paints and Coatings The coatings industry relies heavily on solvents to dissolve resins and pigments. Solvent-based paints and coatings allow for improved application properties, such as spreadability and drying time. However, the environmental impact of volatile organic compounds (VOCs) found in many solvents has led to an increased demand for water-based and green alternatives.
- Cleaning Products Solvents are key components in many cleaning agents, enabling the removal of dirt, oil, and grease from surfaces. Solvents like isopropyl alcohol and acetone are commonly used because of their effective solvent properties. Amidst growing environmental concerns, there has been a shift towards using biodegradable solvents or those with a lower toxicity profile.
Environmental and Health Concerns
Despite their vast applications, chemical solvents pose notable environmental and health risks. Many organic solvents are classified as VOCs, contributing to air pollution and posing risks to human health, such as respiratory issues and neurological effects. Regulations have become stricter regarding the use of hazardous solvents, pushing industries towards more sustainable alternatives. The development of bio-based solvents and solvent recovery techniques has gained traction as strategies to mitigate these concerns.
Future of Chemical Solvents
Looking ahead, the future of chemical solvents will likely focus on sustainability and safety. Innovations in solvent technologies aim to reduce their environmental impact while maintaining effectiveness. Research into green chemistry compels scientists to discover and develop new solvents that are less harmful to health and the environment. Additionally, the growing field of solvent-free chemistry is another promising avenue, aiming to reduce reliance on traditional solvents altogether.
In conclusion, while chemical solvents are indispensable in various applications across industries, the emphasis on environmental sustainability and health safety is reshaping the future landscape of solvents. The ongoing advancements in green chemistry and the quest for safer alternatives will continue to influence solvent-use practices, driving innovation and responsibility in chemical manufacturing processes.
-
How to Choose Dimethyl Disulfide DMDS for Industrial UseNewsNov.09,2026
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
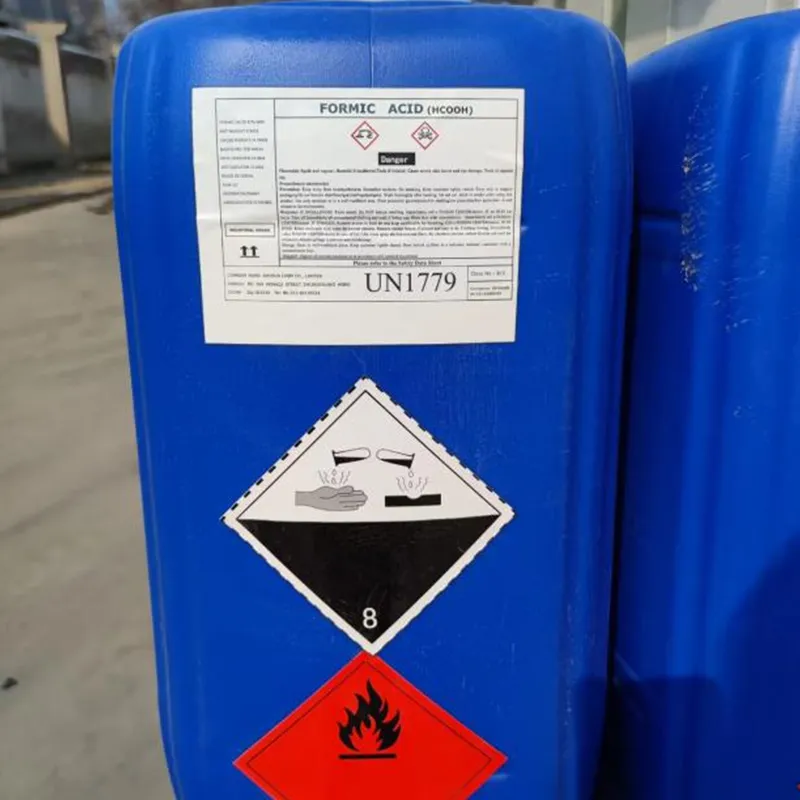
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.