


residual solvents
Understanding Residual Solvents Implications and Importance in Pharmaceuticals
Residual solvents are organic volatile chemicals used during the manufacturing of pharmaceuticals or other chemical products. These solvents remain in the final product, often in trace amounts, after the manufacturing process is completed. Their presence is not merely an incidental byproduct; instead, it carries significant implications for product safety, efficacy, and compliance with regulatory standards.
The use of solvents is common in pharmaceutical processes, including extraction, purification, and crystallization. However, when these solvents are not completely removed, they can pose potential risks to patients. Some residual solvents may be carcinogenic, teratogenic, or otherwise harmful, even in small doses. This risk underscores the necessity for stringent monitoring of residual solvents in pharmaceutical products.
To standardize the evaluation of residual solvents, the International Conference on Harmonisation (ICH) has established guidelines, particularly in the ICH Q3C document. This guideline categorizes solvents into three classes based on their toxicity and potential health risks. Class 1 solvents are to be avoided due to their high toxicity, such as benzene and carbon tetrachloride. Class 2 solvents are less toxic but still require controlled limits, like methylene chloride and ethanol. Class 3 solvents are considered to have low toxic potential and can be used with fewer restrictions, such as acetone and isopropyl alcohol.
The compliance with these guidelines not only ensures product safety but also reinforces a pharmaceutical company's commitment to quality. Regulatory agencies worldwide, such as the U.S. Food and Drug Administration (FDA) and the European Medicines Agency (EMA), enforce strict regulations regarding the allowable limits of residual solvents in finished products. Companies must conduct thorough testing to detect and quantify these solvents, employing methods such as gas chromatography and mass spectrometry. Each batch of pharmaceutical products is subjected to rigorous testing to ensure that it meets the established residual solvent limits.
residual solvents
The process of reducing residual solvents is multifaceted. Manufacturers often implement various strategies to minimize solvent use during manufacturing. This can include optimizing reactions to reduce solvent consumption, employing solvent recovery systems, and adopting greener chemistry practices that utilize less hazardous materials.
In recent years, there has been a growing emphasis on sustainability within the pharmaceutical industry. This reflects broader societal concerns over environmental impact and health risks associated with chemical manufacturing. Consequently, there is an increasing push for the development of more efficient synthesis routes that require fewer volatile solvents or utilize alternative, less harmful solvents.
Furthermore, educating stakeholders about the importance of managing residual solvents is vital. Pharmaceutical companies, suppliers, and even end-users must understand the implications of residual solvents. Awareness of residual solvents can lead to better practices in manufacturing and handling pharmaceuticals, ultimately protecting public health.
In conclusion, residual solvents are a critical aspect of pharmaceutical manufacturing that cannot be ignored. Their presence in pharmaceutical products necessitates strict adherence to safety guidelines and regulatory standards. With ongoing advancements in manufacturing techniques and a growing emphasis on sustainability, the pharmaceutical industry is continually seeking to reduce the reliance on harmful solvents. The ultimate goal remains clear to ensure the safety, efficacy, and quality of the medications provided to patients while promoting a healthier environment.
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
-
Sustainable Agriculture Guide using bio organic fertilizerNewsJun.25,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
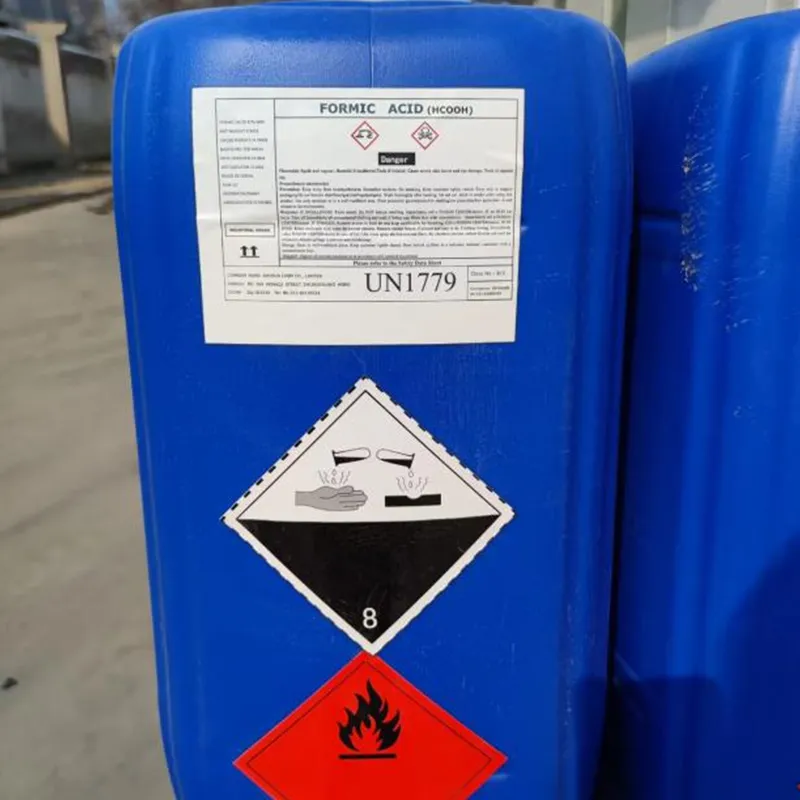
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.