


sbr chemical
Understanding SBR Chemical A Key Player in the Synthetic Rubber Industry
Synthetic rubber has vastly transformed the landscape of modern manufacturing, and among its diverse array of formulations, Styrene-Butadiene Rubber (SBR) stands out as a pivotal component. SBR, a copolymer made from styrene and butadiene, has garnered widespread acceptance in various applications due to its versatility, resilience, and cost-effectiveness. This article delves into the intricate world of SBR, exploring its properties, production processes, applications, and the future outlook of this indispensable material.
The Properties of SBR
SBR is characterized by a unique amalgamation of physical and chemical properties that make it suitable for a myriad of applications. One of its most notable attributes is its excellent abrasion resistance, which enables products made with SBR to endure wear and tear over prolonged use. Additionally, SBR exhibits remarkable tensile strength and elasticity, allowing it to be stretched and compressed without losing its structural integrity.
Moreover, SBR has good thermal stability, making it a reliable choice in varying temperature conditions. Its chemical resistance adds another layer of value, providing protection against certain oils, fats, and other chemicals that could potentially degrade alternative materials. The combination of these properties positions SBR as an ideal component for products in industries that demand durability and reliability.
Production Processes of SBR
The production of SBR typically involves the emulsion polymerization process, where styrene and butadiene monomers are combined in the presence of an emulsifier and an initiator. The process can be conducted under various conditions, yielding different molecular weights and properties based on the desired end application.
SBR can be produced in several grades, each tailored for specific applications. For instance, SBR 1500 is characterized by its high mechanical strength and is commonly used in tires, while SBR 1700 offers improved abrasion resistance and is preferred for manufacturing industrial products. The adaptability of the SBR production process allows manufacturers to fine-tune the properties of the rubber to meet the requirements of specific applications.
sbr chemical

Applications of SBR
The versatility of SBR translates into a wide range of applications across various sectors. One of the most significant uses of SBR is in the automotive industry, particularly in tire manufacturing. SBR is a key ingredient in tire tread formulations, where its durability and resistance to cracking, abrasion, and aging help enhance tire performance and lifespan.
Beyond the automotive sector, SBR finds extensive use in producing conveyor belts, gaskets, seals, footwear, and various molded goods. The footwear industry, for example, relies on SBR for its cushioning properties and flexibility, making it a preferred choice for athletic shoes and casual wear. Moreover, the textile industry utilizes SBR as a coating material, enhancing the durability of fabrics.
The Future of SBR Chemical
As global demands for synthetic rubber continue to grow, the SBR market is poised for significant advancements. Researchers are exploring greener and more sustainable production methods to reduce the environmental impact associated with synthetic rubber manufacturing. Innovations such as bio-based SBR, derived from renewable resources, are gaining traction, aligning with the broader push towards sustainability within the materials industry.
Furthermore, the ongoing development in the automotive sector towards electric vehicles (EVs) poses both challenges and opportunities for SBR. The shift to EVs may influence tire formulations, prompting manufacturers to explore novel compounds that enhance energy efficiency while retaining the essential properties of SBR.
Conclusion
SBR is undeniably a cornerstone of the synthetic rubber industry, providing a balance of performance, adaptability, and cost-effectiveness that few materials can match. Its vast range of applications positions SBR as an integral component in numerous sectors, from automotive to industrial manufacturing. As the industry evolves, the ongoing research and innovations surrounding SBR chemical will likely redefine its applications and production methods, paving the way for a more sustainable and efficient future. Embracing these advancements will ensure that SBR remains a vital player in the world of materials technology for years to come.
-
How to Choose Dimethyl Disulfide DMDS for Industrial UseNewsNov.09,2026
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
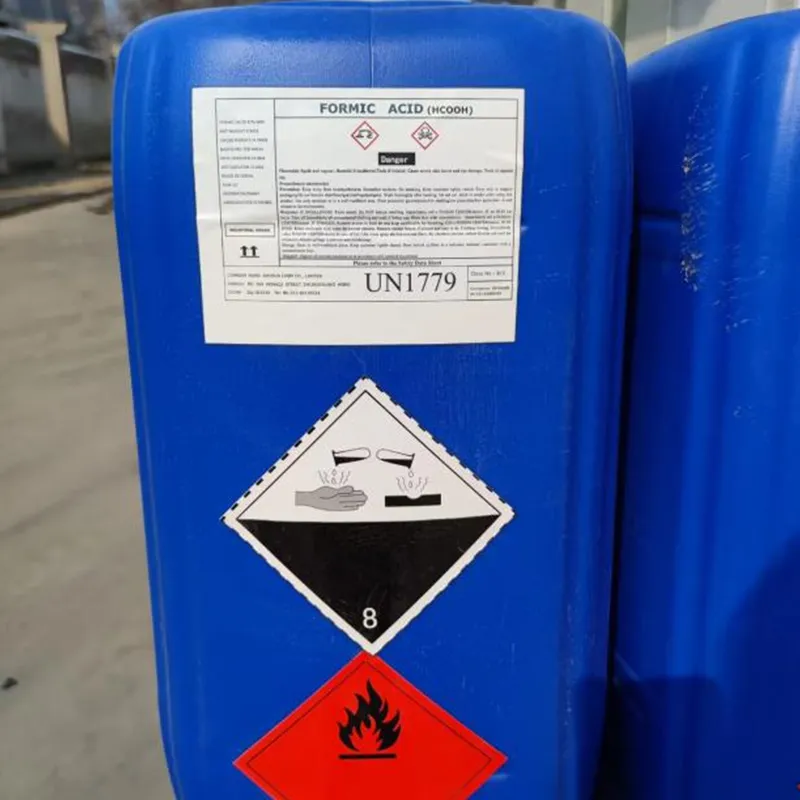
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.