


Analyzing the Properties and Applications of SBR Chemical in Modern Industries
Understanding SBR Chemical Applications and Significance
Styrene-Butadiene Rubber (SBR) is a synthetic polymer that has become a cornerstone material across various industries. Its unique properties and versatility make it an essential chemical compound in many applications. SBR is primarily produced through the polymerization of styrene and butadiene, two petrochemical derivatives. This process yields a rubber-like material known for its resilience, durability, and cost-effectiveness.
Properties of SBR
SBR is characterized by several beneficial properties that contribute to its widespread use. One of its key features is its excellent elasticity, which allows it to stretch and return to its original shape, making it ideal for applications where flexibility is vital. Additionally, SBR possesses good abrasion resistance, tensile strength, and longevity, making it suitable for manufacturing tires, footwear, and various industrial products.
One notable aspect of SBR is its weather resistance and low-temperature flexibility. These properties enable SBR products to maintain performance under various environmental conditions. This adaptability makes SBR a favored choice in the automotive industry, particularly for tire manufacturing, where these characteristics significantly enhance safety and performance on the road.
Applications of SBR
The applications of SBR are diverse, contributing significantly to its prominence in the market. A major application is in the automotive sector, particularly in the production of tires. SBR's ability to withstand wear and tear, coupled with its excellent road holding capability, makes it a material of choice for tire manufacturers. Approximately 40% of the world's SBR production is utilized in tire manufacturing, underscoring its importance in this industry.
sbr chemical

In addition to tires, SBR is widely used in the production of various rubber products. These include conveyor belts, rubber mats, gaskets, seals, and hoses. In the footwear industry, SBR is favored for making shoe soles due to its excellent grip and durability. Moreover, SBR finds applications in the manufacturing of adhesives and sealants, where its properties enhance the performance of these products in different environments.
Another growing application for SBR is in the construction sector. It is increasingly used in the formulation of sealants and coatings, providing weather resistance and durability in construction materials. The ability of SBR to bond well with other materials expands its applications in building and infrastructure projects.
Environmental Considerations and Innovations
Despite its advantages, the production and disposal of SBR raise environmental concerns. The synthesis of SBR involves petrochemical feedstocks, which can contribute to environmental degradation and carbon emissions. Consequently, the industry has seen a push towards developing more sustainable practices. Innovations include the use of bio-based alternatives and improved recycling methods for SBR products at the end of their lifecycle.
Companies are increasingly investing in research to develop greener alternatives, seeking to maintain the performance and cost-effectiveness of SBR while reducing its environmental footprint. These advancements are crucial steps toward aligning the synthetic rubber industry with global sustainability goals.
Conclusion
In summary, SBR chemical is a vital material that plays an integral role in numerous industries, particularly automotive, construction, and consumer goods. Its exceptional properties, including elasticity, durability, and resistance to wear, make it an ideal choice for various applications. However, as the world moves toward greater sustainability, continuous research and innovation will be essential to enhance the environmental performance of SBR and its derivatives. The future of SBR will likely involve balancing its industrial utility with ecological responsibility, ensuring that it remains a valuable resource while minimizing its impact on the planet.
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
-
Sustainable Agriculture Guide using bio organic fertilizerNewsJun.25,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
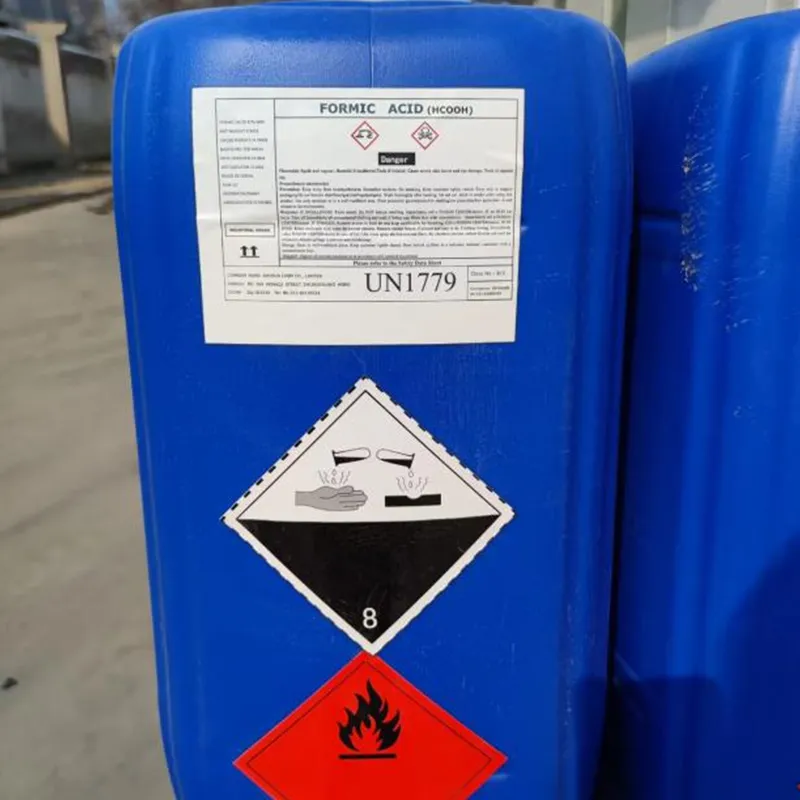
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.