


Aspartame Production Facility Overview and Key Insights
The Aspartame Factory Innovation in Sugar Alternatives
In recent years, the food industry has witnessed a remarkable shift towards healthier options, particularly in sweeteners. Among these alternatives, aspartame has gained significant attention due to its ability to provide a sweet taste while containing virtually no calories. The production of aspartame, primarily at specialized aspartame factories, plays a crucial role in meeting the rising demand for sugar substitutes in various food and beverage products.
Understanding Aspartame
Aspartame is an artificial sweetener that is approximately 200 times sweeter than sucrose (table sugar). Composed of two amino acids—phenylalanine and aspartic acid—this low-calorie sweetener was first discovered in 1965 by chemist James M. Schlatter, while he was researching treatments for ulcers. Since then, it has been extensively used in a variety of products, ranging from diet sodas and sugar-free gums to yogurt and protein powders.
The Manufacturing Process
The production process of aspartame begins with the careful cultivation and extraction of its component amino acids. Phenylalanine and aspartic acid are usually derived from natural sources. The aspartame factory employs state-of-the-art biotechnological methods to ensure the correct ratios and purity levels of these amino acids.
Once extracted, the amino acids are combined under controlled conditions to synthesize aspartame. This process involves a series of chemical reactions, including esterification, where the two amino acids are bonded together by a methyl ester group. Policing the reaction environment—such as temperature and pH levels—is critical, as it can affect both the yield and purity of the final product.
After synthesis, the aspartame is then subjected to rigorous quality control assessments. These tests ensure that the sweetener meets safety and regulatory standards set by organizations like the U.S. Food and Drug Administration (FDA) and the European Food Safety Authority (EFSA). The process is designed to eliminate any contaminants and ensure the enzyme's activity is optimal while maintaining the desired sweetness profile.
Environmental and Economic Considerations
aspartame factory

Manufacturing aspartame in dedicated factories not only caters to the growing market demand but also emphasizes sustainability in food production. Although the raw materials are derived from natural sources, advancements in biotechnology have significantly reduced the environmental footprint of producing these components. For instance, modern methods often utilize fermentation processes that convert agricultural products into amino acids, minimizing waste and energy consumption.
Moreover, the economic impact of aspartame factories is noteworthy. They create jobs in communities, from factory workers and chemists to supply chain managers and logistics coordinators. As aspartame becomes a staple in the food industry, the factories that produce it contribute to the overall economy through job creation and exports.
Health and Safety
One of the most discussed aspects of aspartame is its health implications. While it has been approved for use in over 100 countries, some individuals express concerns regarding its safety, particularly those with phenylketonuria (PKU), a genetic disorder that makes it difficult for the body to metabolize phenylalanine. Consequently, aspartame-containing products are required to carry warning labels for those with this condition.
Ongoing research continues to assess the long-term effects of aspartame consumption. However, numerous studies have indicated that aspartame is safe for the general population when consumed within established acceptable daily intake levels. The consensus among health authorities is that aspartame can be part of a balanced diet, especially for individuals seeking to reduce their sugar intake.
The Future of Aspartame
Looking ahead, the future of aspartame production remains promising. As consumer preferences continue to evolve towards healthier options, aspartame factories are well-positioned to adapt and innovate. Research into new methods of production, potential new formulations, and blends with other sweeteners could further enhance the appeal and application of aspartame in various culinary creations.
In conclusion, the aspartame factory is at the forefront of a pivotal change in the food industry. Through innovative production techniques, strict safety measures, and a focus on sustainability, these facilities play a vital role in producing a sweetener that aligns with modern health-conscious consumer lifestyles. As the demand for sugar alternatives grows, so too will the significance of aspartame and its manufacturing processes in shaping a healthier future.
-
How to Choose Dimethyl Disulfide DMDS for Industrial UseNewsNov.09,2026
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
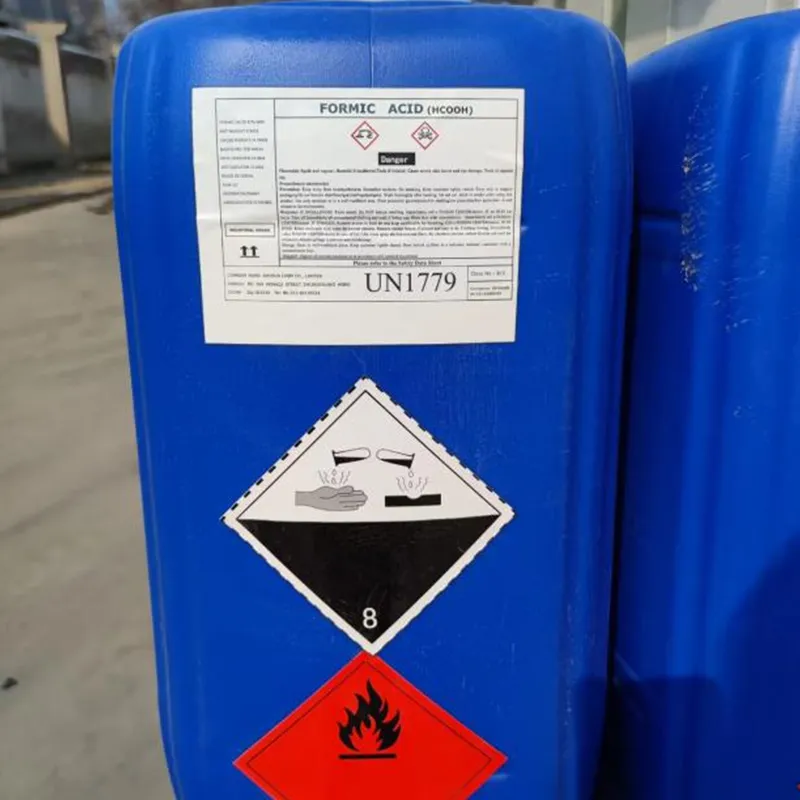
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.