


Exploring the Advantages and Applications of Brominated Butyl Rubber in Modern Industries
Brominated Butyl Rubber An Overview of Properties, Applications, and Benefits
Brominated Butyl Rubber (BIIR) is a specialized synthetic rubber that has gained significant attention in various industries due to its unique properties and versatile applications. It is a halogenated variant of butyl rubber, which is known for its impermeability, resilience, and chemical resistance. The introduction of bromine into the butyl rubber structure enhances its flame retardancy and offers several other benefits that make it suitable for a wide range of uses.
One of the key characteristics of brominated butyl rubber is its excellent resistance to heat, ozone, and aging. This makes it an ideal choice for products that are exposed to harsh environmental conditions. The bromination process alters the rubber's chemical structure, providing enhanced thermal stability and making it less susceptible to degradation over time. As a result, BIIR is often used in applications where longevity and reliability are paramount, such as in automotive tires, seals, and gaskets.
In addition to its durability, brominated butyl rubber is also recognized for its low permeability to gases and liquids. This feature is particularly important in industries where maintaining vacuum or preventing contamination is critical. For example, BIIR is commonly utilized in the manufacture of inner linings for tires, where its barrier properties help to retain air pressure and improve fuel efficiency. This characteristic is also beneficial in the production of inflatable products and various medical devices.
The flame retardant nature of brominated butyl rubber is one of its most significant advantages. The presence of bromine acts as a barrier to combustion, making it an excellent choice for applications that require enhanced fire safety. This includes the production of electrical insulation materials, conveyor belts, and automotive components that must comply with fire safety regulations. The use of BIIR in these applications not only improves safety but also can lead to reduced insurance costs and liability for manufacturers.
brominated butyl rubber

Moreover, brominated butyl rubber is compatible with a variety of other materials, which allows for the development of composite products possessing desirable traits from multiple sources. This compatibility opens the door for innovative applications in sectors such as construction and consumer goods. The rubber can be blended with other polymers or fillers to create materials tailored for specific performance requirements, enhancing its utility across diverse applications.
Another notable application of brominated butyl rubber is in the medical field. Its biocompatibility and ability to provide a sterile barrier make it suitable for the production of rubber stoppers, seals, and other medical devices. These products often require stringent compliance with health and safety standards, and the properties of BIIR help manufacturers meet these regulations effectively.
Despite its many benefits, the production and use of brominated butyl rubber also raise environmental considerations. The halogenated nature of brominated compounds has led to scrutiny given their potential impact on human health and ecosystems. However, advancements in manufacturing processes and recycling methods are helping to address these concerns. Manufacturers are increasingly adopting sustainable practices, and ongoing research is focused on developing bromine derivatives that minimize environmental impact while maintaining desirable material properties.
In conclusion, brominated butyl rubber is a remarkable material that combines durability, flame retardancy, and low permeability, making it valuable across various industries. Its applications range from automotive and construction to medical and consumer goods, showcasing its versatility. As research progresses and sustainability practices evolve, the future of brominated butyl rubber appears promising, continuing to offer innovative solutions while addressing environmental challenges. With its essential properties and adaptability, BIIR is poised to maintain its significance in the world of materials science for years to come.
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
-
Sustainable Agriculture Guide using bio organic fertilizerNewsJun.25,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
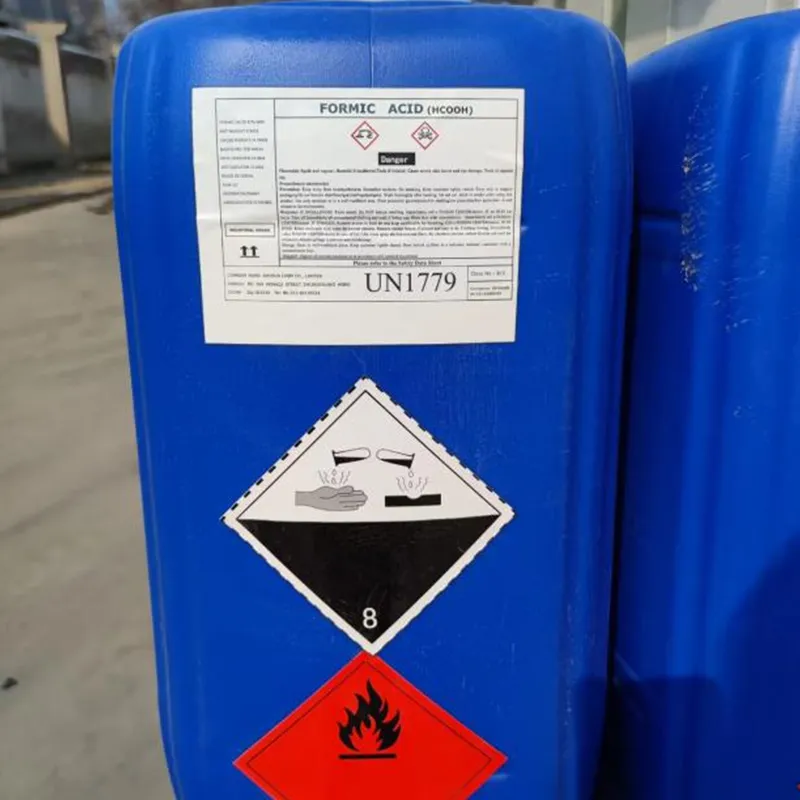
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.