


Exploring the Applications and Benefits of Fluorinated Solvents in Various Industries
The Role of Fluorinated Solvents in Modern Applications
Fluorinated solvents are a specialized category of solvents characterized by the presence of fluorine atoms in their chemical structure. These compounds have gained significant attention in various industries due to their unique properties, which distinguish them from conventional organic solvents. This article explores the characteristics, applications, environmental considerations, and future trends related to fluorinated solvents.
Characteristics of Fluorinated Solvents
Fluorinated solvents possess unique physical and chemical properties that make them highly effective in various applications. One of the most notable features is their exceptional thermal and chemical stability. The carbon-fluorine bond is one of the strongest in organic chemistry, making these solvents less reactive and more stable across a wide range of temperatures and pH levels. This stability provides an advantage in processes that involve harsh conditions, enabling them to maintain their effectiveness without decomposing or reacting undesirably with other materials.
Another defining characteristic of fluorinated solvents is their low surface tension and high volatility. These traits allow for efficient penetration into complex geometries and intricate components when used in cleaning applications. Furthermore, many fluorinated solvents exhibit low global warming potential (GWP) compared to traditional chlorinated solvents, adding an environmental benefit to their use.
Applications of Fluorinated Solvents
Fluorinated solvents have found diverse applications across several industries, including electronics, pharmaceuticals, and aerospace. In the electronics industry, they are often employed as cleaning agents for delicate components, such as circuit boards and optical devices. Their ability to evaporate quickly without leaving residues makes them ideal for cleaning and maintaining high precision instruments.
In the pharmaceutical sector, fluorinated solvents are utilized in extraction and synthesis processes. Their unique properties can enhance the solubility of certain compounds, making them ideal for developing new drugs or extracting active ingredients from natural sources. Moreover, they serve as reaction media for various chemical processes, providing a controlled environment for reactions to occur efficiently.
fluorinated solvents

The aerospace industry also benefits from fluorinated solvents, where these compounds are used for de-greasing processes that ensure the reliability and safety of aircraft components
. Their effectiveness in penetrating oils and greases while remaining chemically stable enhances the maintenance of aerospace equipment.Environmental Considerations
Despite their advantages, the use of fluorinated solvents is not without concerns. Some fluorinated compounds, particularly those containing perfluorinated chemicals (PFCs), have been scrutinized for their environmental impact. Certain PFCs have been linked to serious ecological and health concerns due to their persistence in the environment and potential to bioaccumulate in living organisms.
To address these issues, regulations are being developed in many regions to limit or phase out the use of harmful fluorinated solvents. This has prompted researchers and companies to seek alternative solvents that are more environmentally friendly while maintaining effectiveness in their respective applications. Increasingly, industries are focusing on the development of next-generation fluorinated solvents that minimize environmental impact while maximizing performance.
Future Trends
The future of fluorinated solvents is poised for significant evolution, driven by technological advancements and regulatory changes. Innovations in synthetic methods may yield new fluorinated compounds that are less harmful to the environment, while research into the effectiveness of these solvents can lead to enhanced applications in emerging fields such as nanotechnology and green chemistry.
Moreover, as industries continue to prioritize sustainability, there may be a shift toward developing biodegradable or recyclable alternatives to traditional fluorinated solvents. The push for greener chemical processes will likely catalyze an increased interest in solvents that can deliver similar performance without the associated environmental risks.
In summary, fluorinated solvents play a critical role in many industrial applications due to their unique properties and effectiveness. While challenges remain regarding their environmental impact, ongoing research and development efforts hold promise for a more sustainable future, ensuring these specialized solvents can continue to contribute to advancements across various fields. As industries strive for innovation in a more eco-conscious landscape, the evolution of fluorinated solvents remains a fascinating area of study and application.
-
How to Choose Dimethyl Disulfide DMDS for Industrial UseNewsNov.09,2026
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
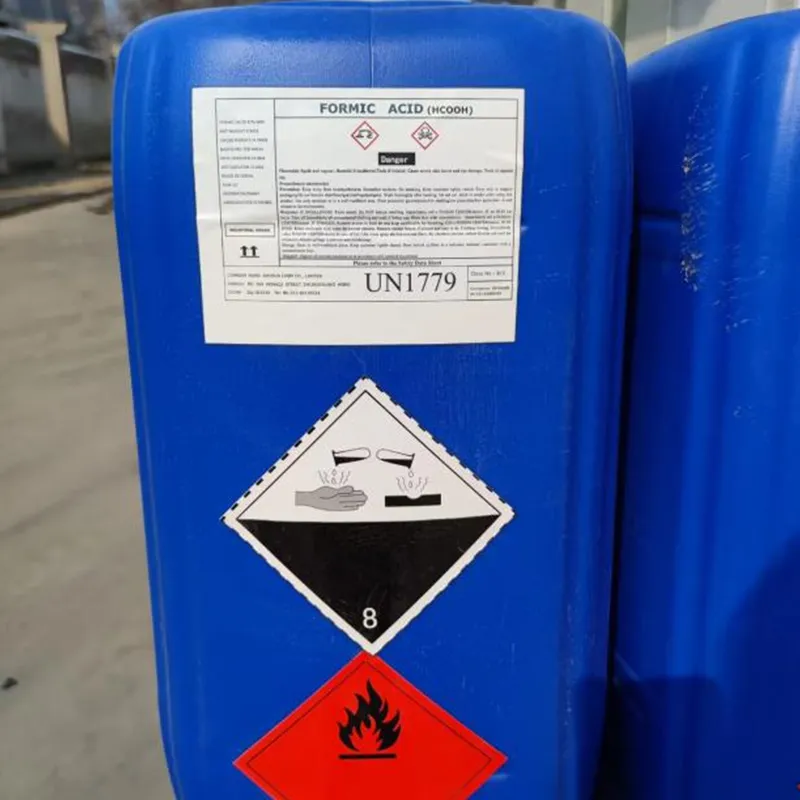
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.