


Nitrile Rubber Applications and Benefits in Various Industries and Products
The Versatility and Applications of Nitrile Rubber
Nitrile rubber, also known as nitrile butadiene rubber (NBR), is a synthetic rubber that has garnered significant attention in various industrial applications due to its unique properties and versatility. Developed in the 1930s, this elastic material is formed by the copolymerization of acrylonitrile and butadiene. The ratio of these two components can be adjusted to optimize specific functional characteristics, making nitrile rubber an ideal choice for a wide range of uses, particularly in environments that require resistance to oils, fuels, and other chemicals.
One of the primary benefits of nitrile rubber is its impressive oil resistance. This makes it a preferred material in industries where exposure to hydrocarbons is prevalent, such as automotive, aerospace, and manufacturing. Nitrile rubber products are commonly used in the fabrication of O-rings, seals, gaskets, and hoses, ensuring that they can withstand the harsh conditions often seen in machinery and automotive engines. These components play a crucial role in preventing leaks and ensuring operational efficiency, which is paramount in mechanical applications.
In addition to its oil resistance, nitrile rubber boasts excellent abrasion resistance and resilience. This property enhances its durability and longevity, particularly in high-wear applications. Many industrial machinery components made from nitrile rubber can withstand significant wear, reducing the frequency of repairs and replacements. Moreover, its high tensile strength allows for effective use in products that require flexibility and elasticity, making it suitable for various molding applications.
Nitrile rubber also performs admirably across a range of temperatures, maintaining their structural integrity in both hot and cold environments. This thermal stability is critical in applications such as fuel systems, where the compound may experience fluctuations in temperature. Additionally, it possesses good compression set resistance, ensuring that it retains its shape and performance over extended periods, making it a reliable option for many sealing applications.
nitrile rubber

Another aspect where nitrile rubber excels is its compatibility with numerous additives and fillers. This allows manufacturers to create customized formulations tailored to specific needs, thereby enhancing its properties for particular applications. For instance, by varying the acrylonitrile content, manufacturers can adjust the rubber’s hardness, flexibility, and resistance to various chemicals. This adaptability is invaluable in designing products for specialized markets.
Beyond its industrial applications, nitrile rubber is also employed in consumer products. Many disposable gloves used in food processing, medical examinations, and other hygiene-sensitive environments are made from nitrile rubber. These gloves provide excellent barrier protection against oils and chemicals while ensuring durability. The increasing awareness of workplace safety standards around the globe has propelled the demand for nitrile gloves, especially in situations where latex allergies are a concern.
Despite its numerous advantages, nitrite rubber does have some limitations. It is not as flexible as some other types of rubber, such as natural rubber, particularly in very low temperatures. This characteristic necessitates a careful consideration of its application environments. Furthermore, while nitrile rubber is highly resistant to oils and fuels, it may not perform as effectively against certain polar solvents or other aggressive chemicals, meaning that careful selection is crucial for applications involving these substances.
In conclusion, nitrile rubber is a robust and versatile material that finds extensive applications across multiple industries. Its unique blend of oil resistance, durability, and flexibility makes it the material of choice for many mechanical components and consumer products. As industries continue to evolve and adapt, the demand for nitrile rubber will likely grow, driven by innovations that enhance its properties and expand its applications. Its significance in both industrial and consumer markets underscores its status as a vital material in contemporary manufacturing and product development.
-
Aspartame Buyer FAQ: Sweetness, Specifications and ApplicationsNewsNov.02,2026
-
Aluminum Hydroxide FAQ: Specifications, Ordering and Support QuestionsNewsOct.28,2026
-
Improve Crop Yield with Premium Calcium Boron FertilizerNewsJul.01,2026
-
Ultimate Guide to Cal Mag Fertilizer for Boosting Plant HealthNewsJun.29,2026
-
Maximize Crop Recovery Using High Performance Bounce Back FertilizerNewsJun.27,2026
-
Maximize Crop Yields and Soil Health with Biozyme FertilizerNewsJun.26,2026
-
Sustainable Agriculture Guide using bio organic fertilizerNewsJun.25,2026
Hebei Tenger Chemical Technology Co., Ltd. focuses on the chemical industry and is committed to the export service of chemical raw materials.
-
view more Tplyltriazole(TTA)Tplyltriazole is a powerful and versatile corrosion inhibitor,it is a white particle or powder that is easily hygroscopic and can be processed into large, small, columnar, fine, or powdered shapes.It is a highly effective solution for preventing rust and corrosion on a variety of metal surfaces, making it an ideal choice for a wide range of applications. -
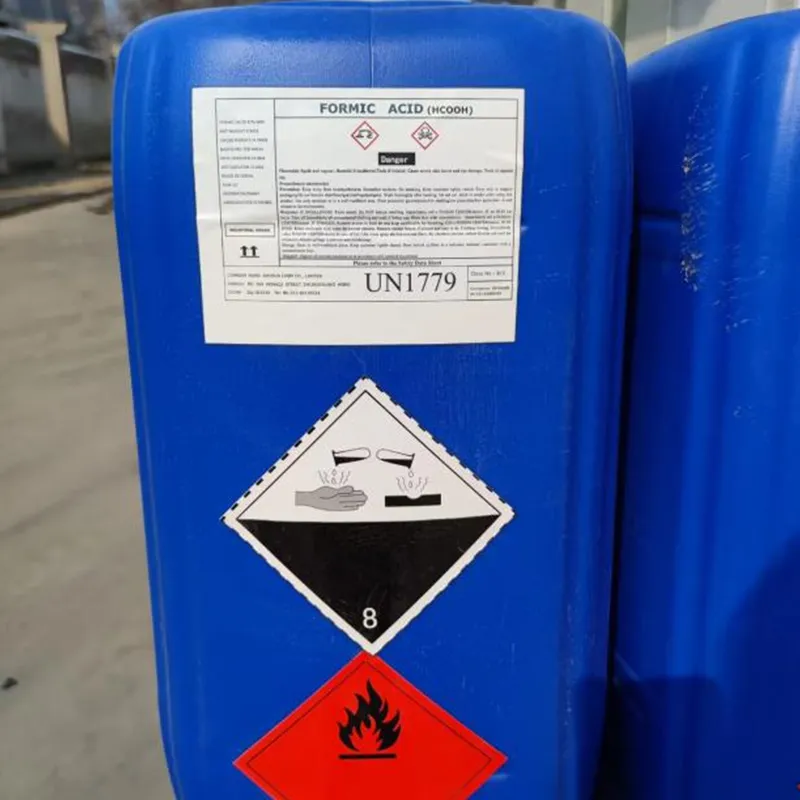
view more Formic AcidFormic acid, is a colorless, pungent-smelling liquid.With its unique properties and diverse applications that serves a wide range of industrial and commercial applications. -
view more Aluminum HydroxideAluminum Hydroxide, a versatile and essential product for a wide range of applications.This product is a white, amorphous powder that is insoluble in water and has a variety of uses in industries such as pharmaceuticals, cosmetics, and manufacturing.